EMS-Trade
Cooling
Loop consumables

Document ECT-01 · REV C · ISSUED 2026-09 Six lines · 48 sheets

Sheet 02 · About · the supply network behind six lines

One interface in front of a supply network

We do not run a factory. The six product lines on this site are made on supplier lines we have inspected, and every part reaches you through one interface: one specification, one certificate pack, one address that answers.
Request the specification file One business day, with the file attached

Metal parts EN 10204 3.1 Cleanliness target ISO 4406 17/15/12 Samples 7–10 days Production 25–35 days

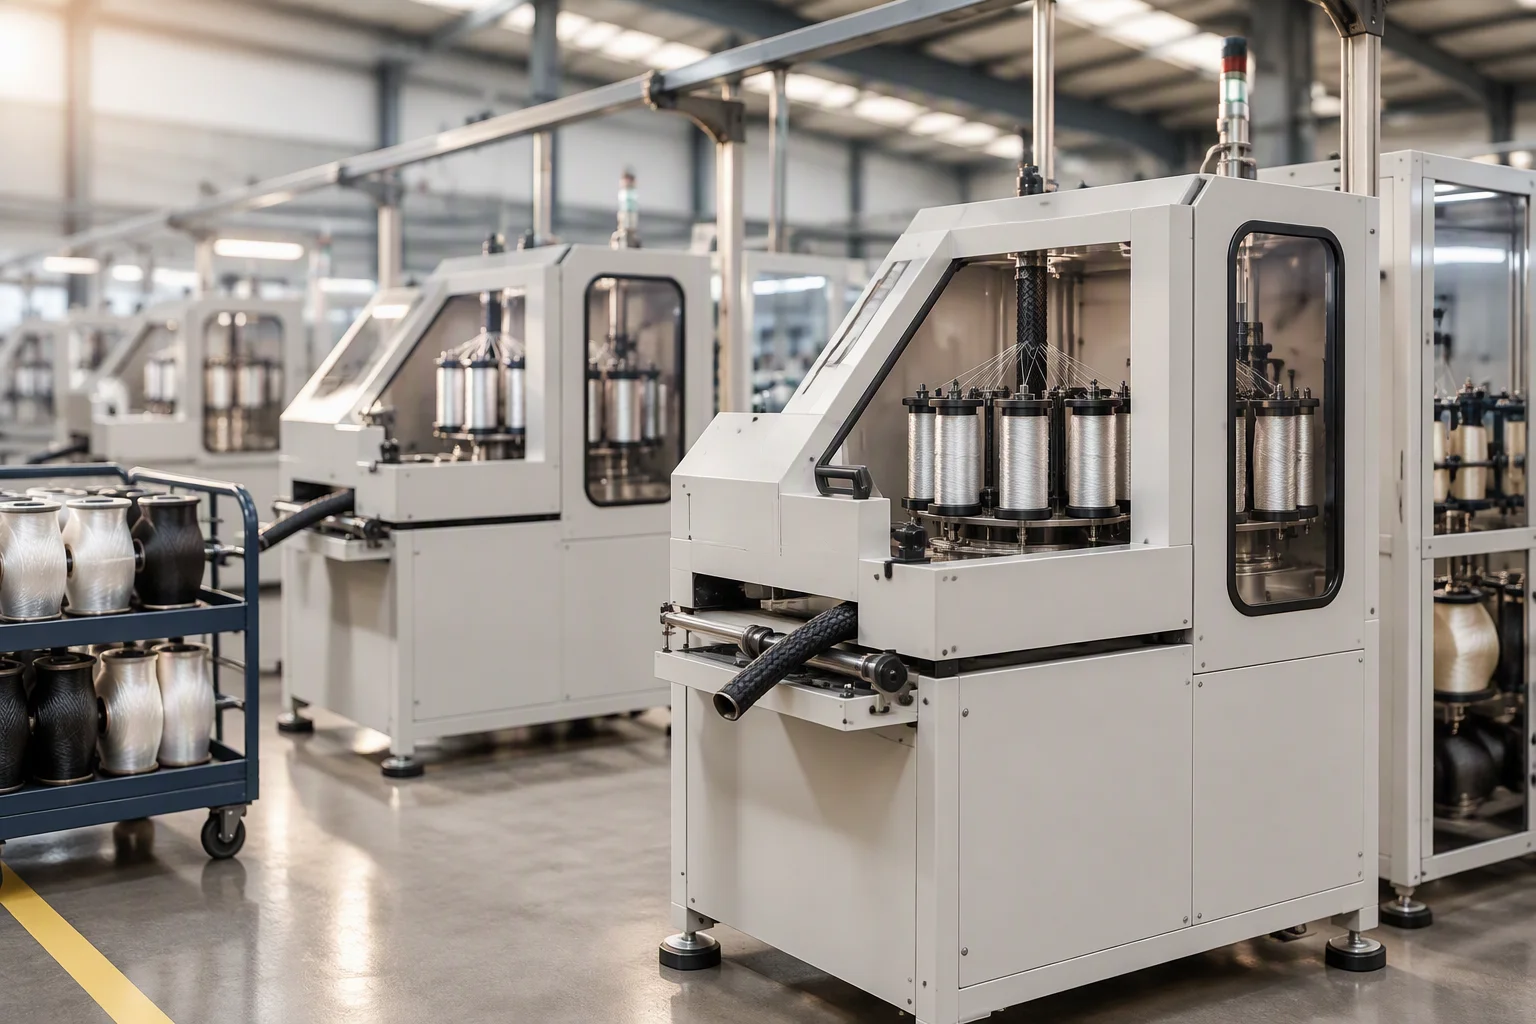
Braiding machines in a bay, bobbins of synthetic fibre on the carrier rings and hose being covered at the centre
FIG 01

· A braiding bay our orders run through. It is a supplier's line, not ours.

01

A supply network, not a factory

Position · what the buyer is actually dealing with

A liquid cooling loop is bought as one system and maintained as many parts. Housings, hose, seals, sensing rope and instruments come from different workshops, and the buyer carries the job of making them agree with each other. That job is what this sheet takes over.

Six lines are held to one specification, one cleanliness target and one packing standard. What changes for you is the number of interfaces: drawings, certificates and shipping documents arrive from one place, against one document number, instead of six.
Role
Supplier of the loop itself: filtration, leak detection, hose and piping, thermal materials, telemetry, fill and flush.
Not supplied
The coolant distribution unit and the cold plate. Both are designed and warranted by their own makers.
Where parts are made
On the lines of five specialised suppliers in China, one per product line. Each line is inspected before it is quoted, and re-inspected per batch after that.
Who installs it
The contractor of record. Installation, system design and commissioning are not offered here, and nothing on this site commits to them.
A machine room floor beside a cable route, the slab and the services that run across it
FIG 02

· The parts live under the tiles. Anything supplied has to survive there.
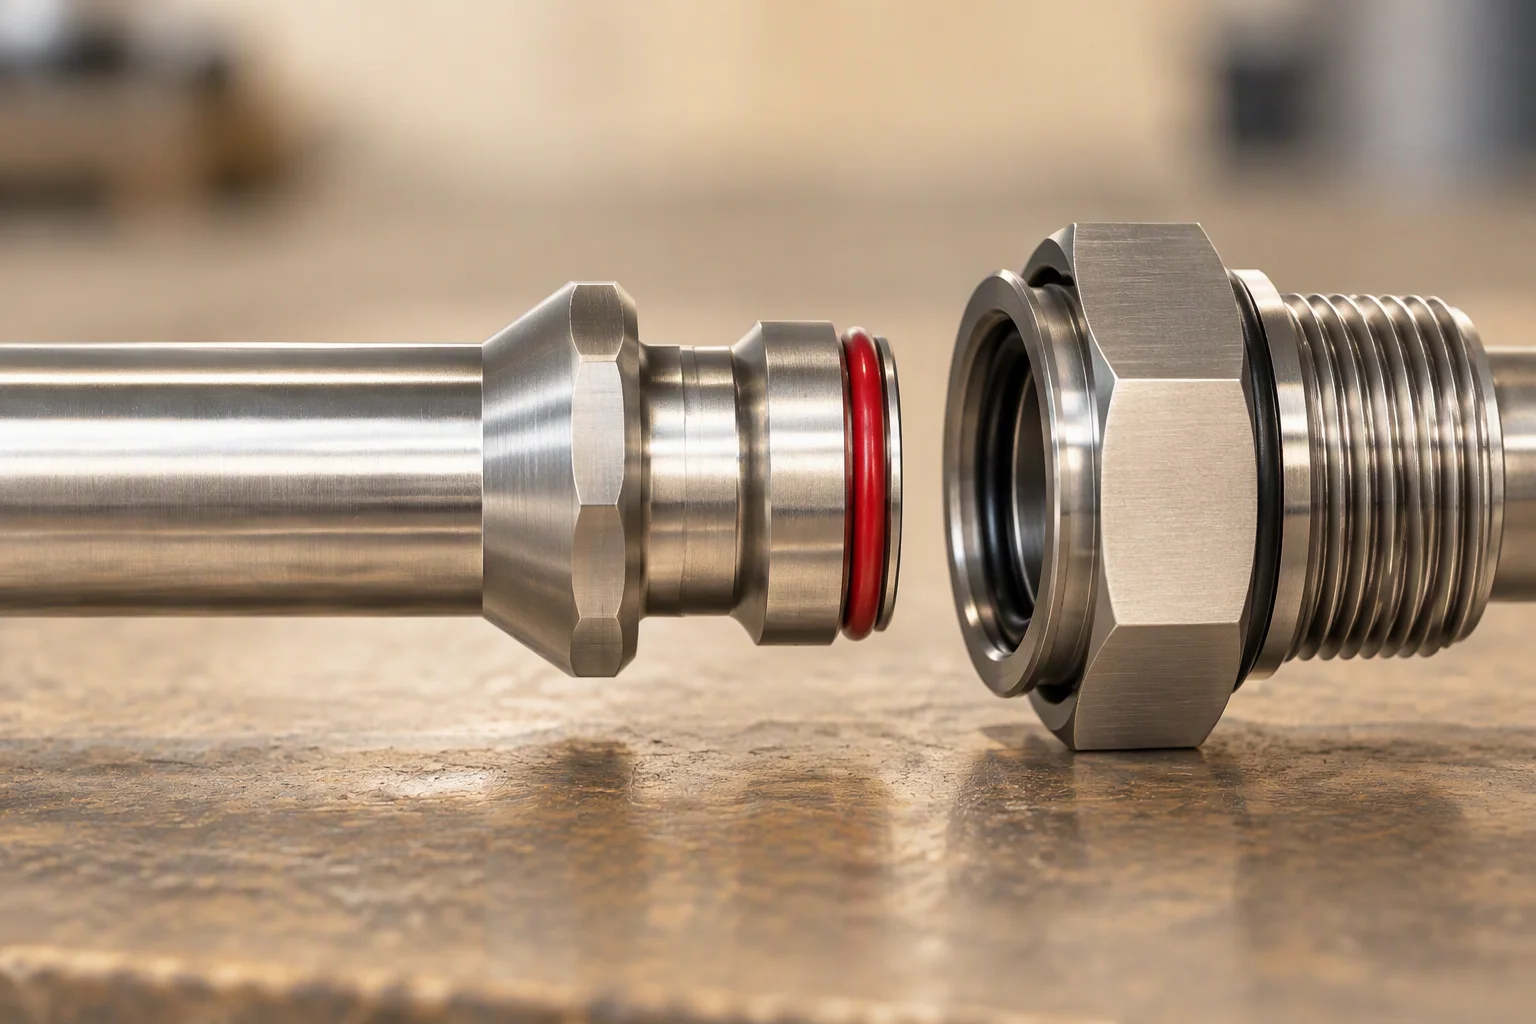
Two fittings brought together on a bench, the seal face and the groove visible at the joint before make-up
FIG 03

· One interface, cut to one drawing, whether the part came from bay one or bay six.

02

Every line, and the figure that decides it

Schedule A · six lines · one decisive figure each

Six product lines · what is supplied · the figure that decides the line · the interface it is held to
Line Supplied Decisive figure Interface
Leak detectionLine 01 Locating sensing rope, point sensors, controllers, end terminations 500 m per channel Modbus RTU · dry contact
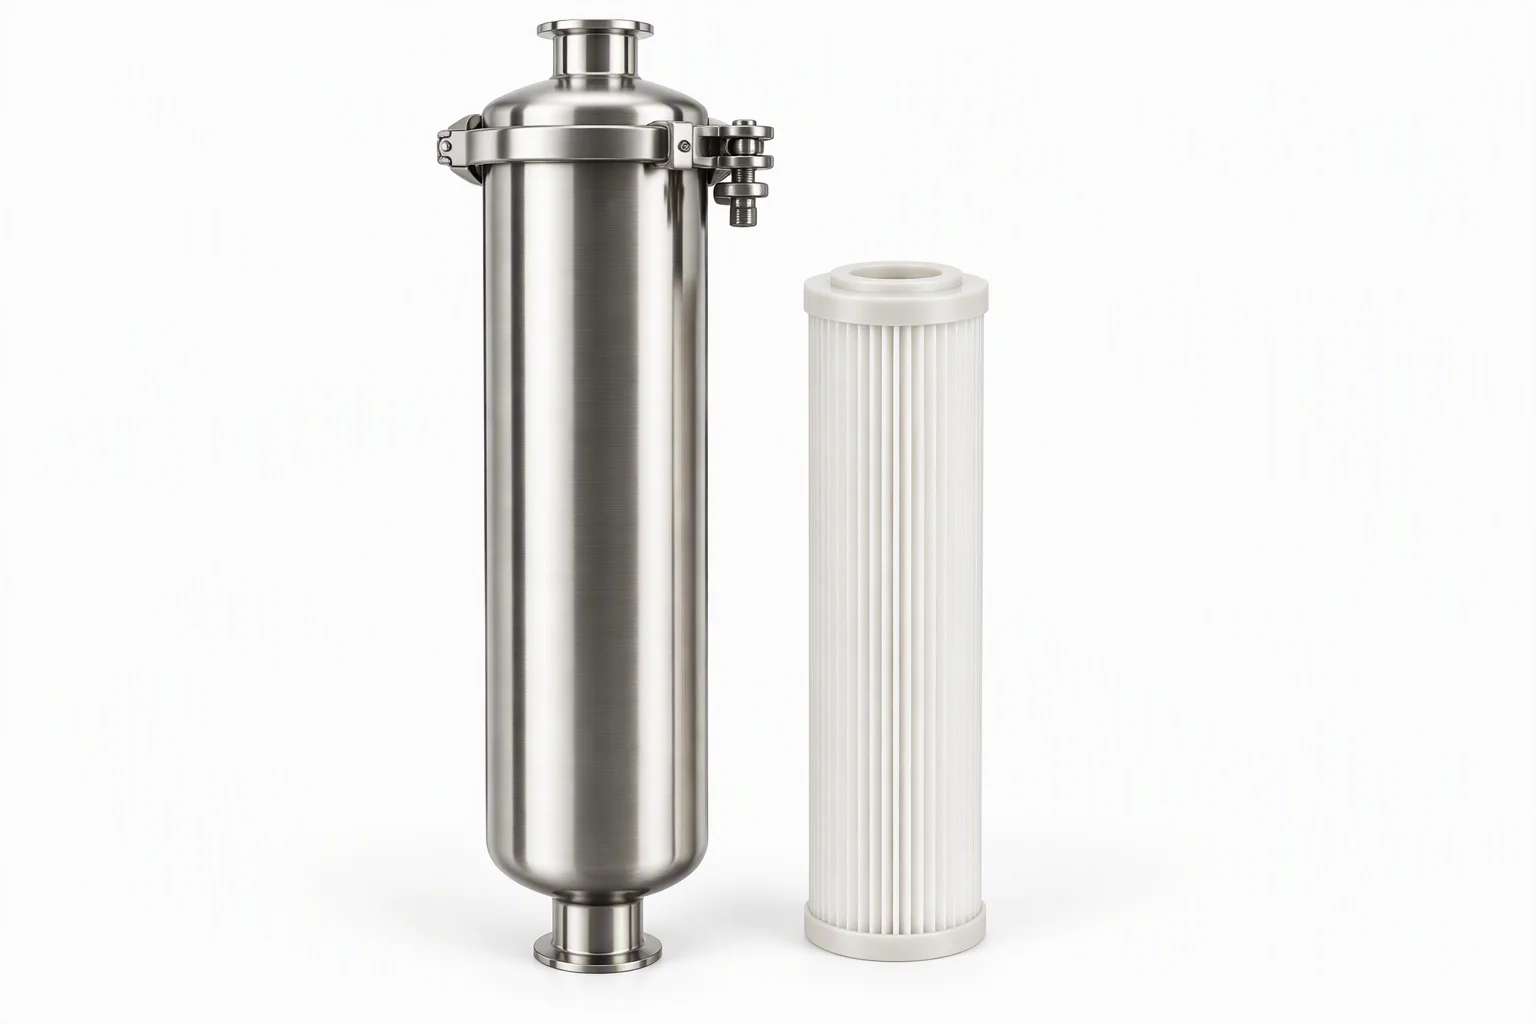
Coolant filtrationLine 02 Housings, cartridges, and the in-line water quality transmitters 1 µm absolute ISO 4406 17/15/12
Hose and pipingLine 03 EPDM hose assemblies, metal fittings, quick disconnects 1.38 MPa ≈ 200 psi UQD · DASH −4 to −10
Thermal materialsLine 04 Grease, gap filler pads, phase change material, graphite sheet 1.0–15.0 W/m·K Bond line · pump-out
Telemetry instrumentsLine 05 Flow, differential pressure, level, conductivity and pH instruments 4–20 mA Modbus RTU · dry contact
Fill and flushLine 06 Service carts, filtration units, sampling points, target cleanliness ISO 4406 17/15/12 Two-stage filtration

Figures are the ones the line is quoted on. Line 02 is quoted at the 1 µm grade; the other seven cartridge grades are quoted per size. Line 06 is quoted against the cleanliness target, not against a volume.
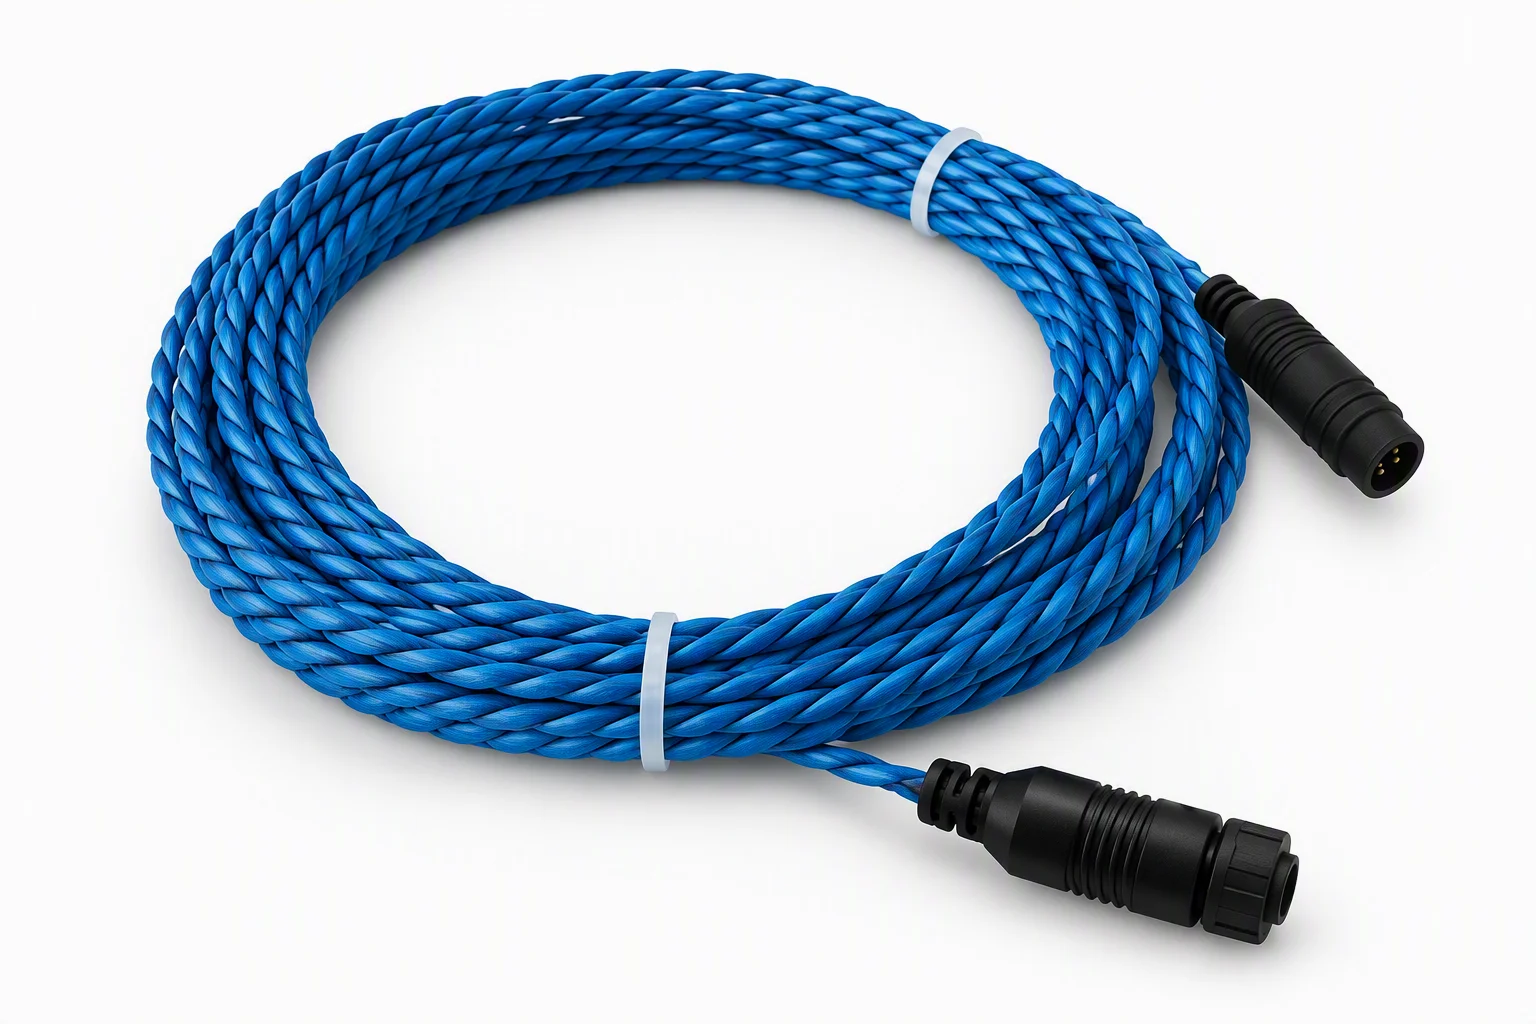
Coil of braided locating sensing rope with its termination plug laid beside it on a white catalogue ground
Line 01 · Leak detection 500 m per channel
Stainless filter housing standing beside its pleated cartridge, both upright on a white catalogue ground
Line 02 · Coolant filtration 1 µm absolute
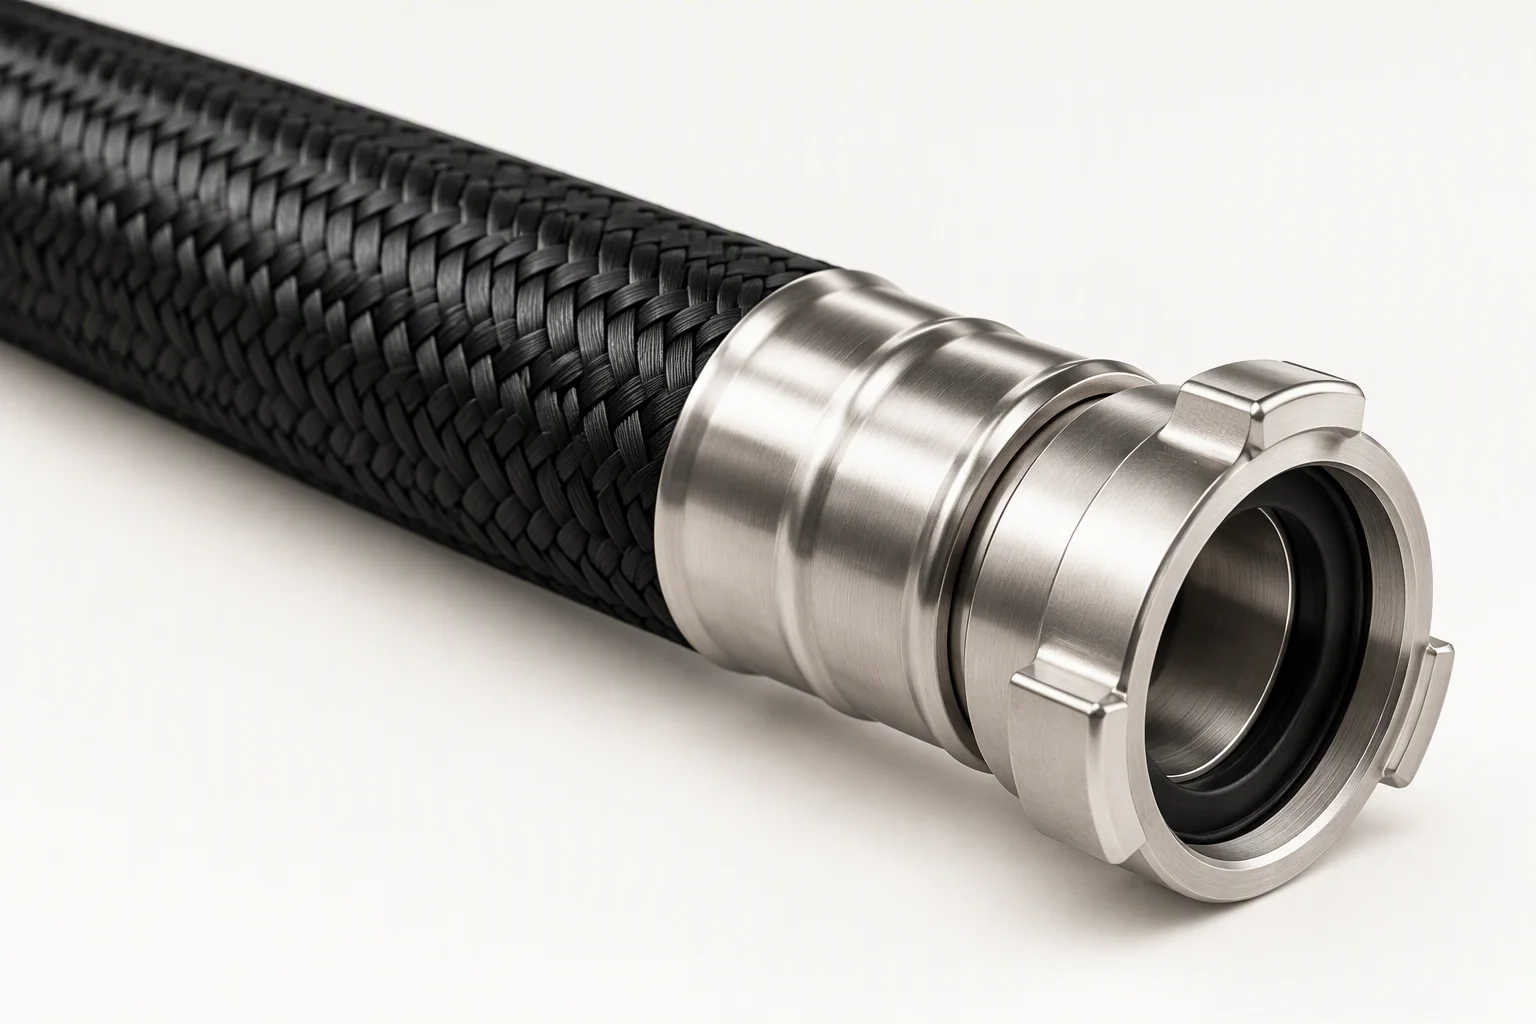
Black braided EPDM hose cut to length with a crimped stainless coupling at the end, the seal face showing
Line 03 · Hose and piping 1.38 MPa ≈ 200 psi
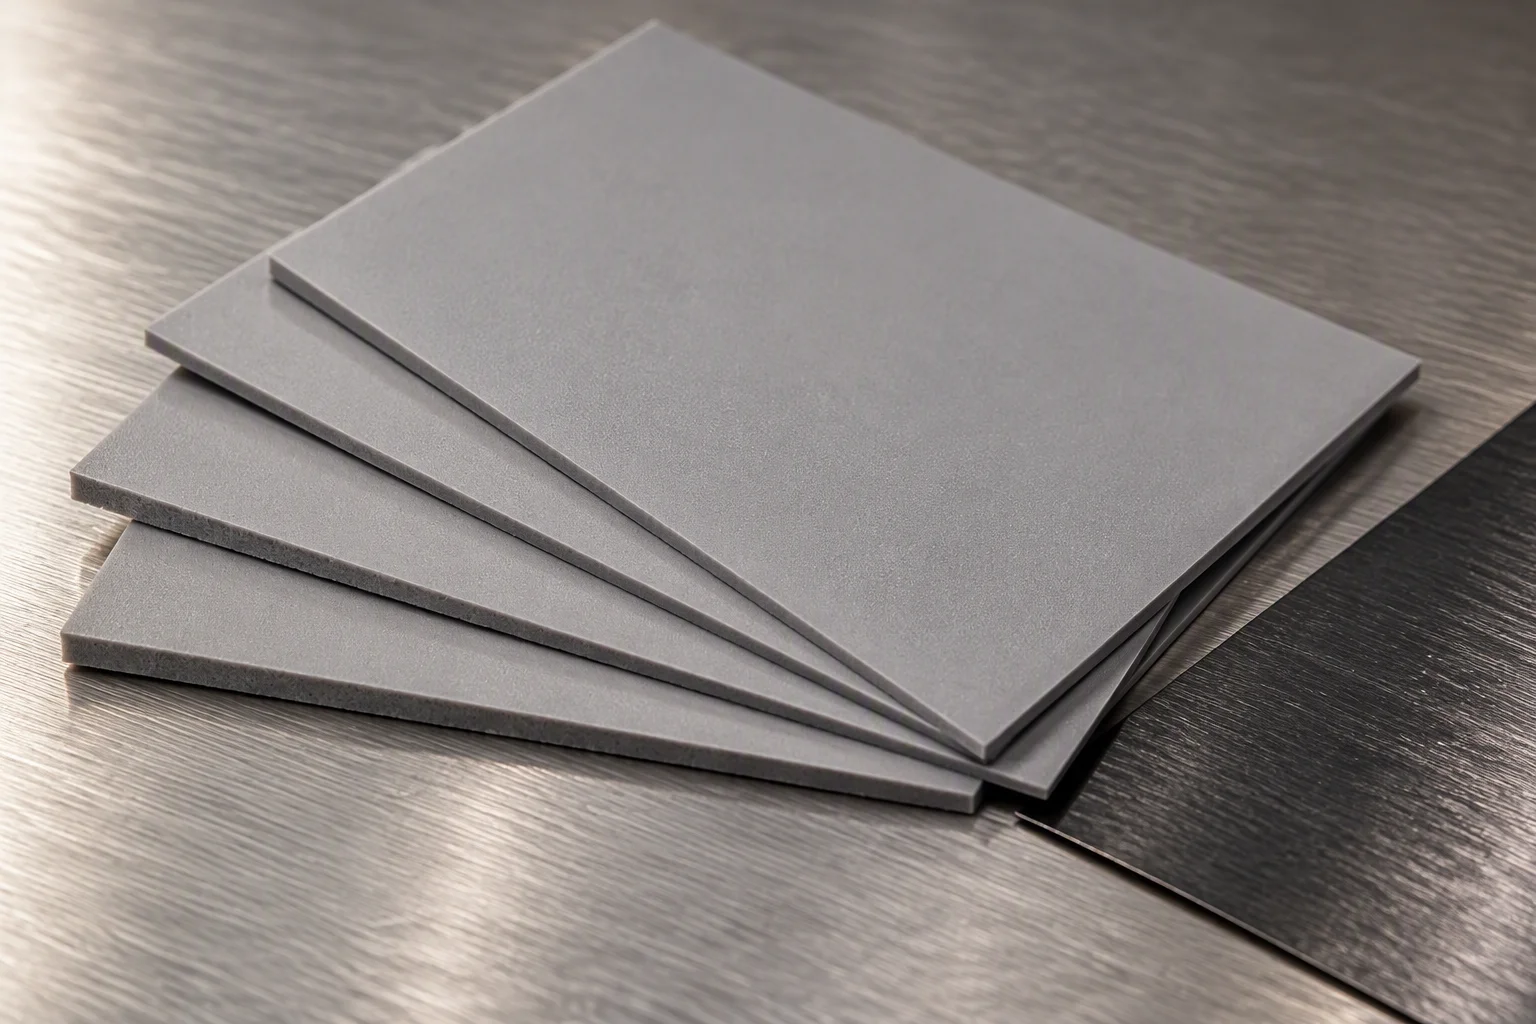
Grey gap filler pads and a dark graphite sheet fanned across a brushed metal surface, cut edges showing thickness
Line 04 · Thermal materials 1.0–15.0 W/m·K
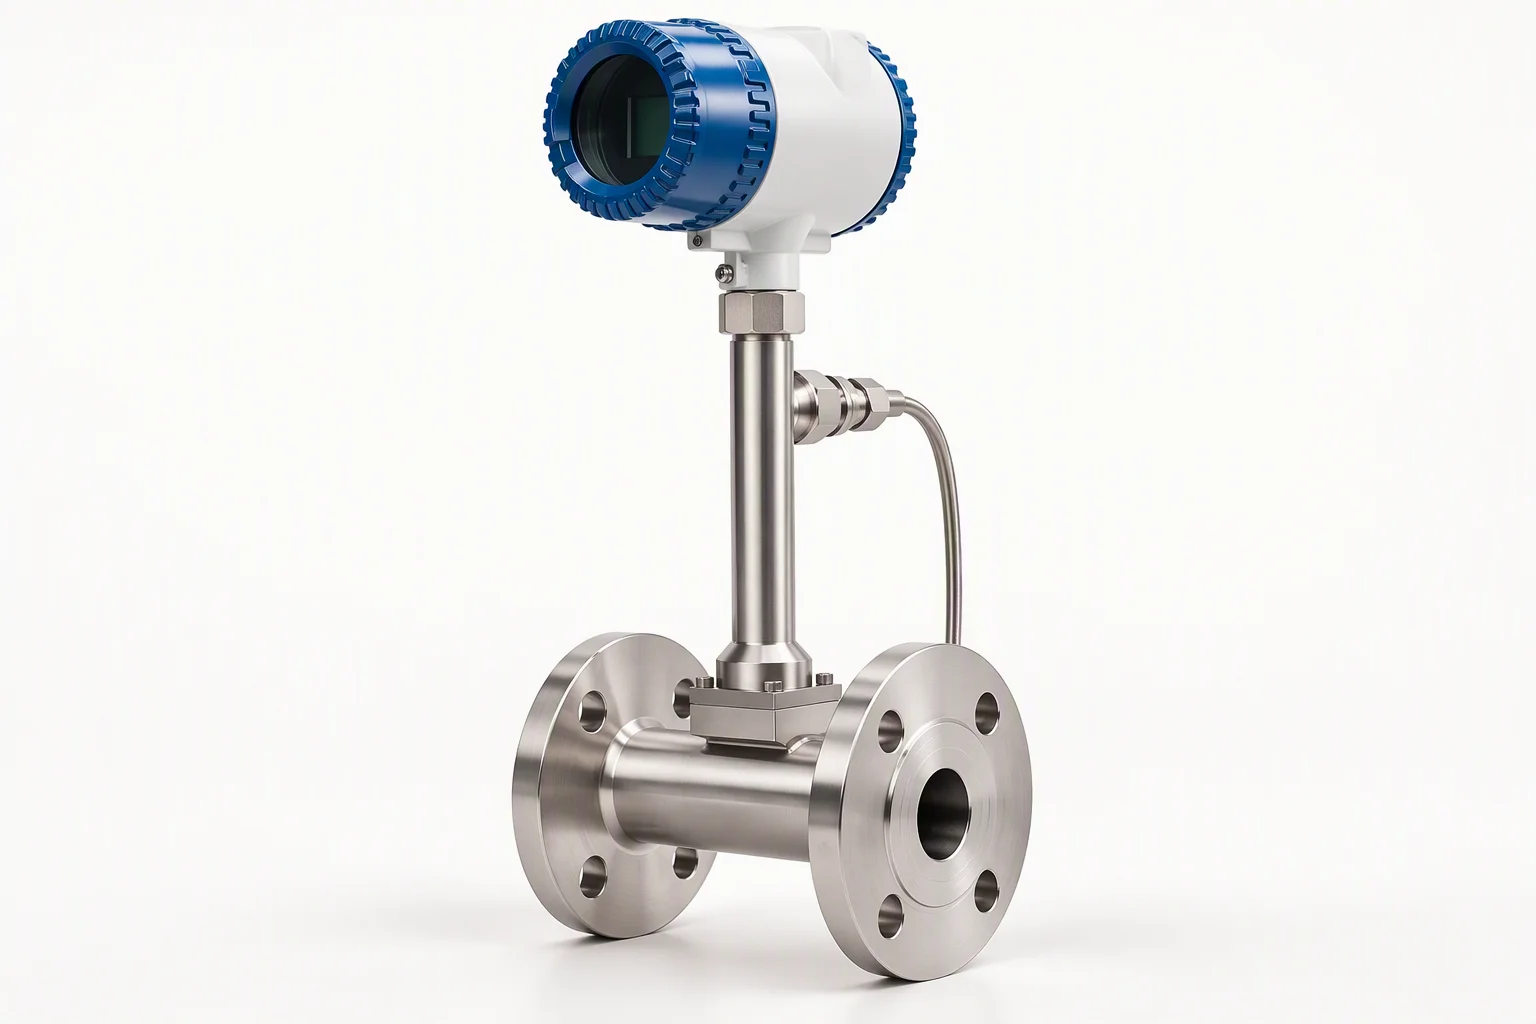
In-line flow meter body in stainless with its display head turned to the walkway, cable gland at the base
Line 05 · Telemetry 4–20 mA
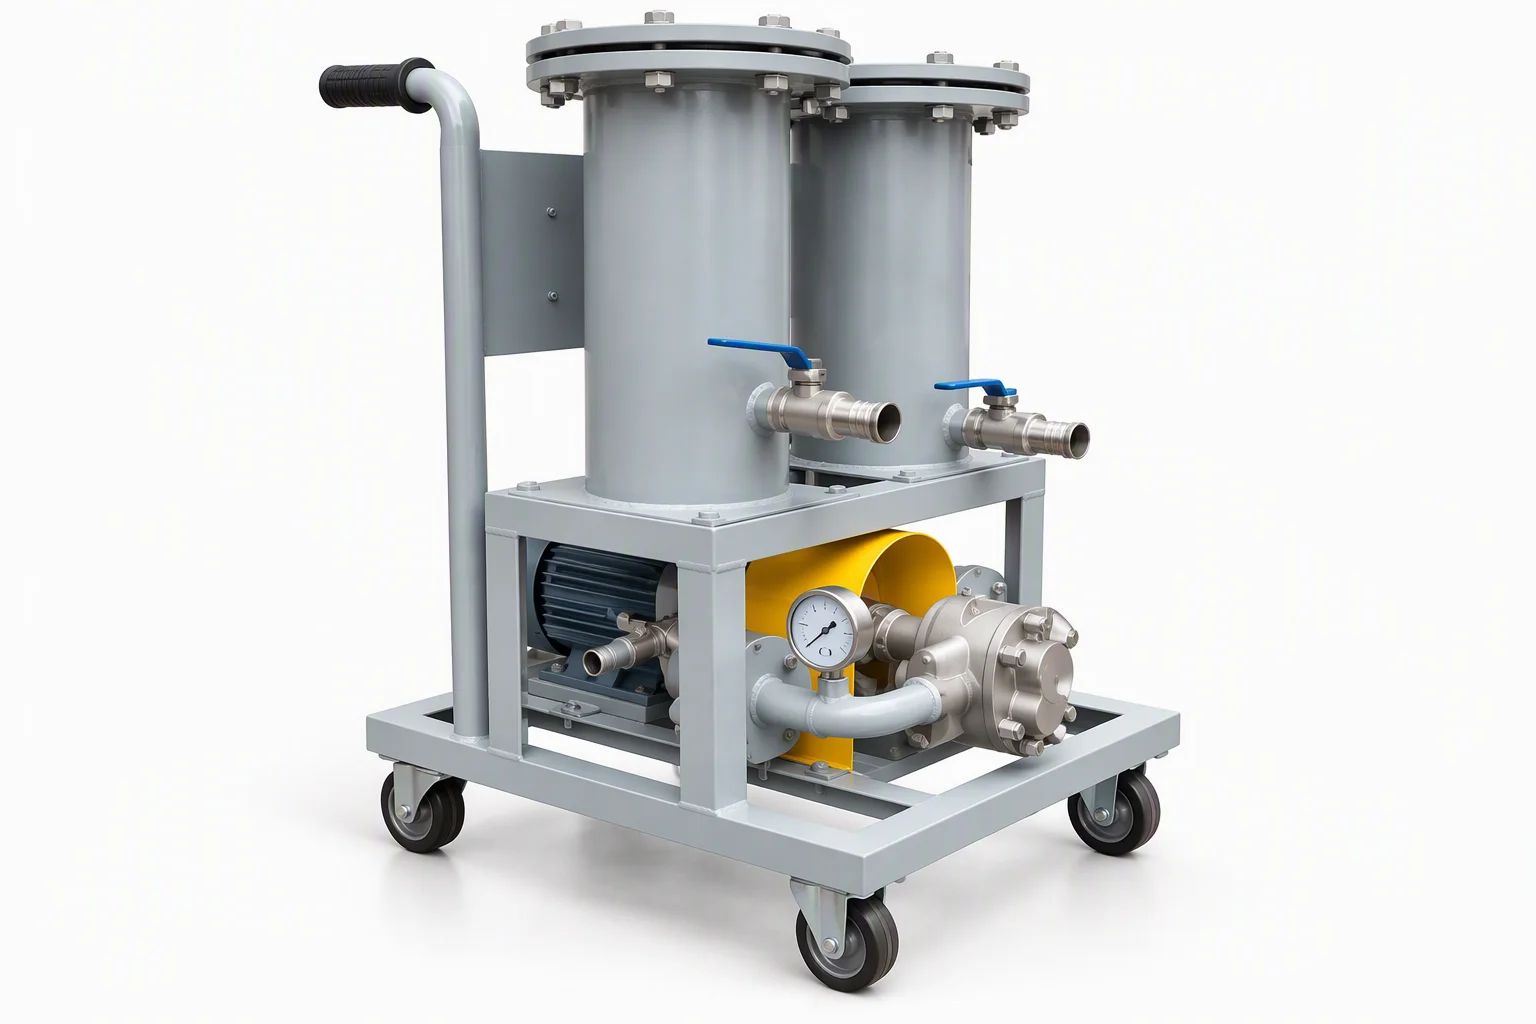
Mobile two-stage filtration cart: two grey housings with flanged lids, ball valves, a pump and a pressure gauge on casters
Line 06 · Fill and flush ISO 4406 17/15/12

One mount per line, at the size the line is quoted at. Links to the full schedule of each line are in the index at the top of this sheet.

03

The interface, in three parts

Thread and face · seal · proof

Thread and face
Threads and seal faces are cut to the outline drawing issued with the quotation, so a part from one bay makes up with a part from another. Metal parts carry EN 10204 3.1 certificates.
Seal
The elastomer is called out on the same drawing as the metal: profile gasket, O-ring, or bonded seal. A seal is never substituted for stock without a new drawing number.
Proof
Hose assemblies are proof-tested at the working pressure of 1.38 MPa and burst-tested to ≥ 5.5 MPa. Filter housings are tested to ≥ 1.0 MPa before dispatch.
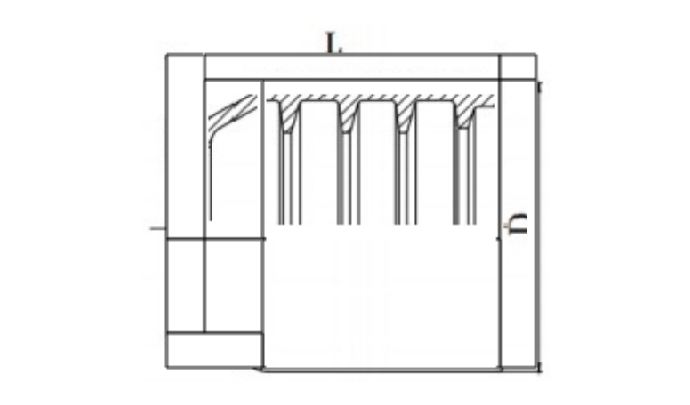
Section drawing of a fitting with the overall length and the bore called out as L and D, hatched cut faces and no lettering
DRG 01

· A cut fitting from the quotation pack. Length and bore are the only two call-outs.
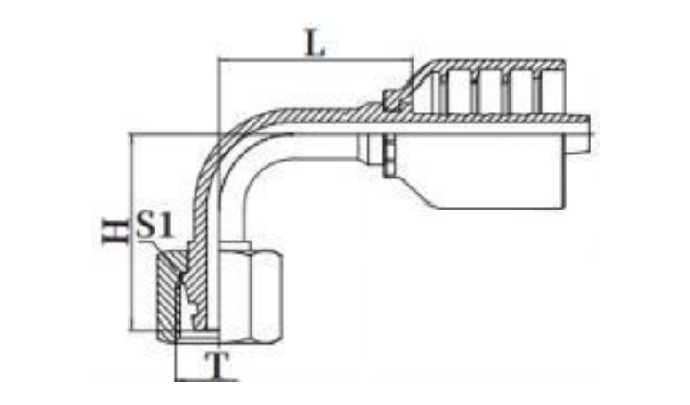
Section drawing of a ninety degree elbow fitting, the bend and the hex flats shown in section with H, S1, L and T call-outs
DRG 02

· The same interface turned through ninety degrees, with the hex flats dimensioned.
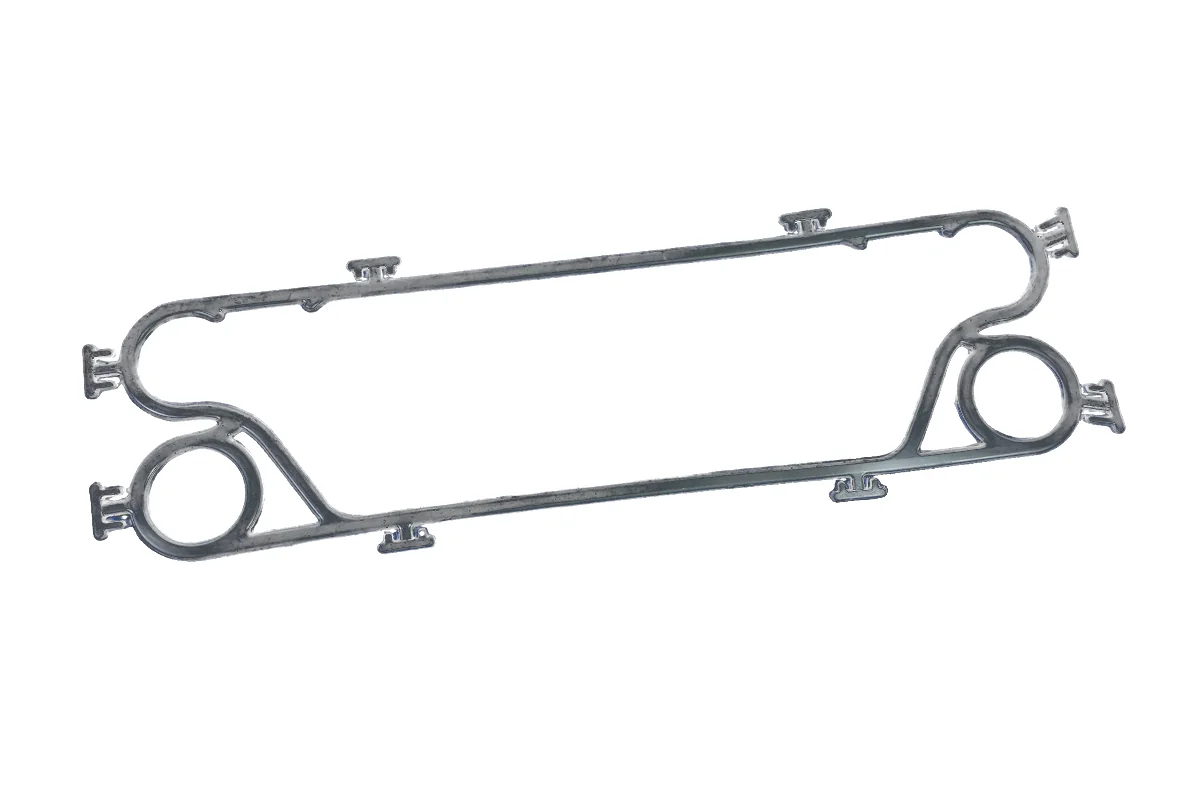
A moulded elastomer profile gasket photographed on a light ground, its locating clips and moulded corners seen edge on
PL 01

· A moulded profile gasket. The seal is drawn, not matched by eye at the bench.

04

Inspection, and the record that follows the part

Four checkpoints · one record per batch

A part is only as good as the batch it came out of. Every line runs the same four checkpoints, and every one of them writes a line into the record that ships with the goods.

  • Incoming material: grade, hardness and dimensional check against the drawing
  • In process: torque, seal face and thread gauges on the parts that make up
  • Before dispatch: pressure proof, plus a burst sample per hose batch
  • Records: certificate, test report and packing list raised against one document number
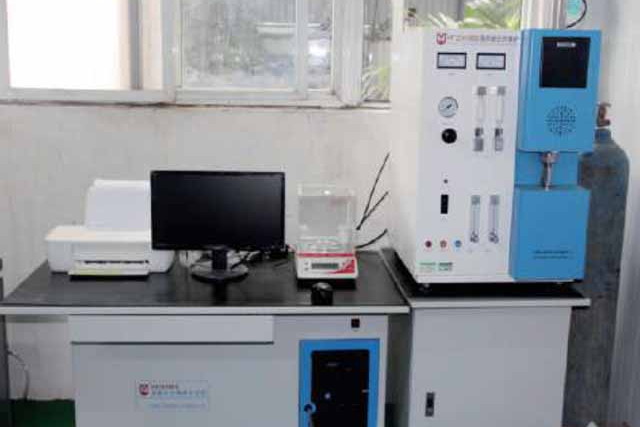
The inspection bench: two instrument consoles with the sample position between them
FIG 04

· Incoming material is measured against the drawing, not against the last delivery.
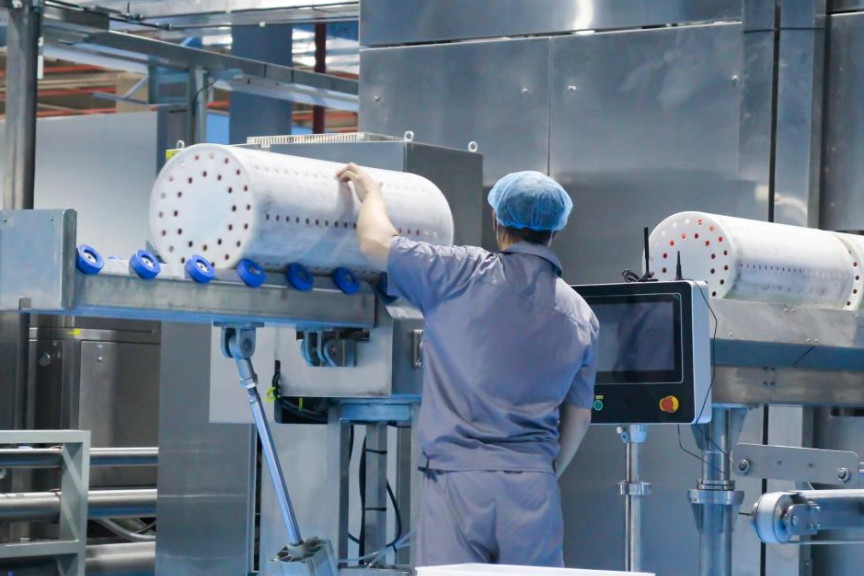
An operator at a tube assembly station, back to the camera, fitting a length into the housing
FIG 05

· The piece the record is raised against: one assembly, one batch, at the station it was built on.
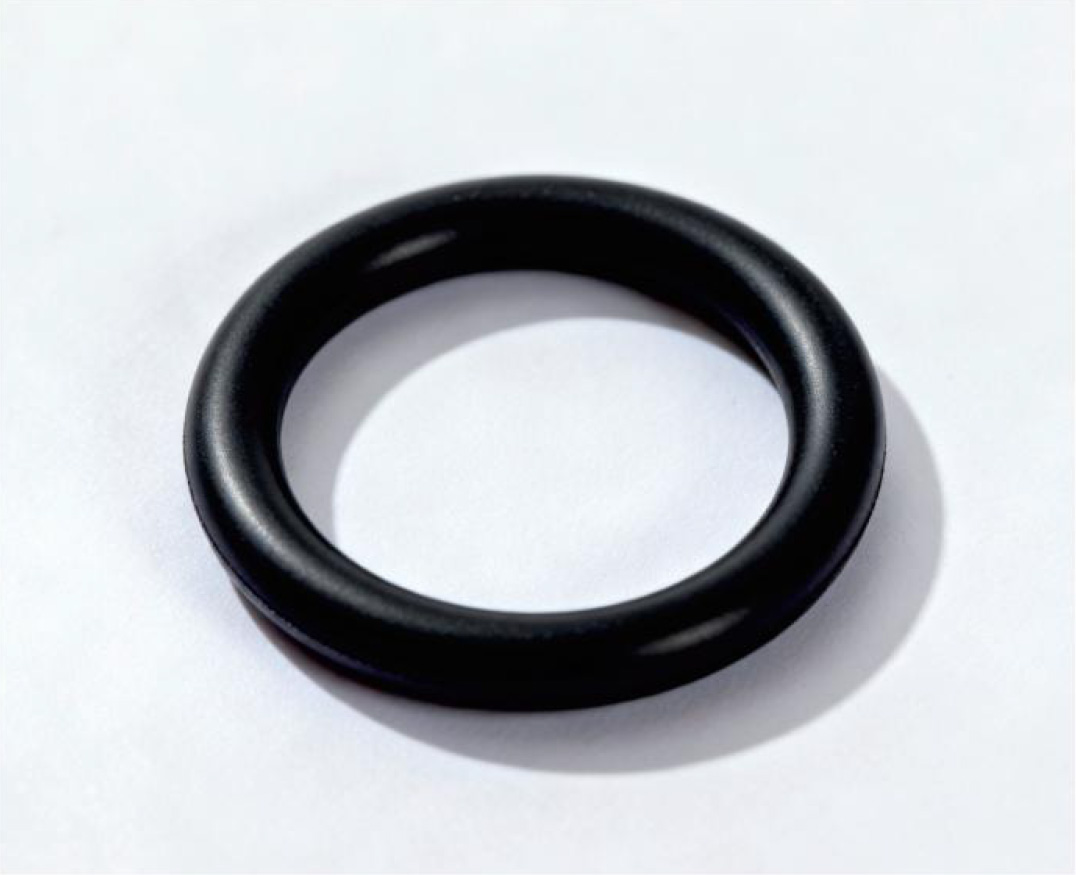
A single black O-ring photographed on a light ground, the moulding seam visible along the inner face
PL 02

· An incoming O-ring. Hardness and cross section are measured, not assumed from the part number.
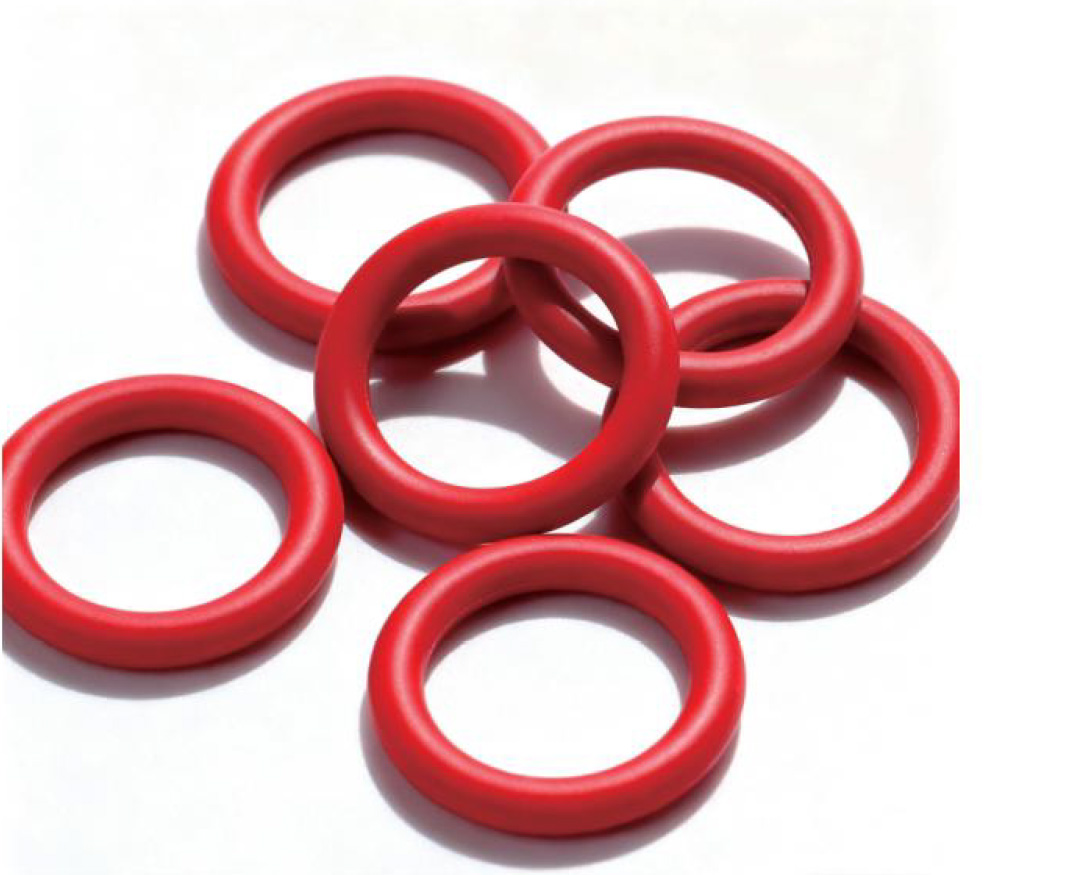
Six red O-rings of one size arranged on a white ground, each lying flat showing the full cross section
PL 03

· One batch, one size, six pieces. The sample that goes into the record comes off the top of this pile.

Document request

Four documents are held for this sheet. Tick the ones you need.

Tick a document, name the line and the quantity, and the file comes back attached.

The only promise on this page

One business day, with the file attached.

Nothing else on this sheet is promised. Price, stock and lead time are not promised here.
If the form cannot send, the address below takes it instead: sales@ems-cool.com. A request is never accepted and then dropped.
A bound specification file open on a bench, the page showing a ruled drawing of a fitting and its seal
An export desk with a stack of document folders, a sample box and a hose assembly laid on the worktop